
Brand Color Management
Focusing on the full-lifecycle management of brand colors and addressing inconsistencies in packaging colors across different factories, batches, and materials constitutes the core service for enhancing brand visual consistency.
Leveraging a leading industry-specific color expertise team and professional equipment such as EPSON S80680, Techkon SpectroDens, and SpectroDrive, we provide end-to-end services encompassing color data acquisition, algorithm research, standard development, and digital asset creation. We establish a brand-specific color standard parameter library to enable secure storage, efficient sharing, and standardized application of color data, ensuring that brand colors are accurately reproduced across different scenarios and production stages.
Brand Color Standard Establishment Process
Starting with the materials and craftsmanship, first tone down the color, then verify the final effect.
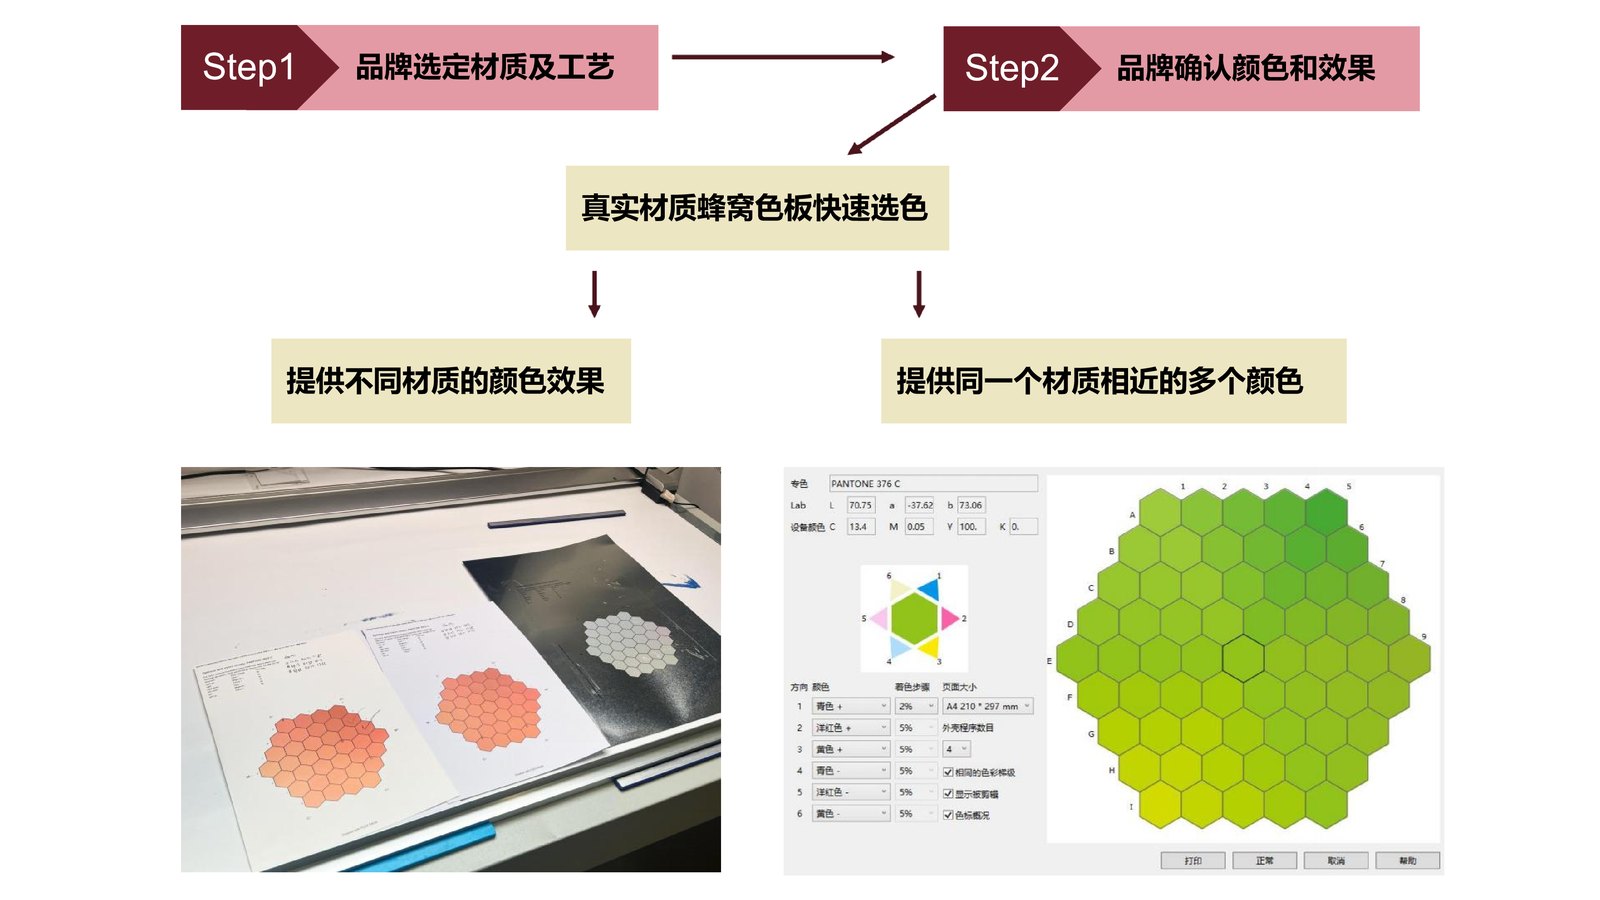
Select materials and craftsmanship for the brand
Provide color effects for different materials, giving a tangible basis for selecting materials and craftsmanship.
Confirm the brand colors and effects
Provide multiple colors based on the same material and similar hue; use a real-material honeycomb color palette for rapid comparison and convergence.
Precise color tracking across materials
Quantitative management of the same spot color across different materials.
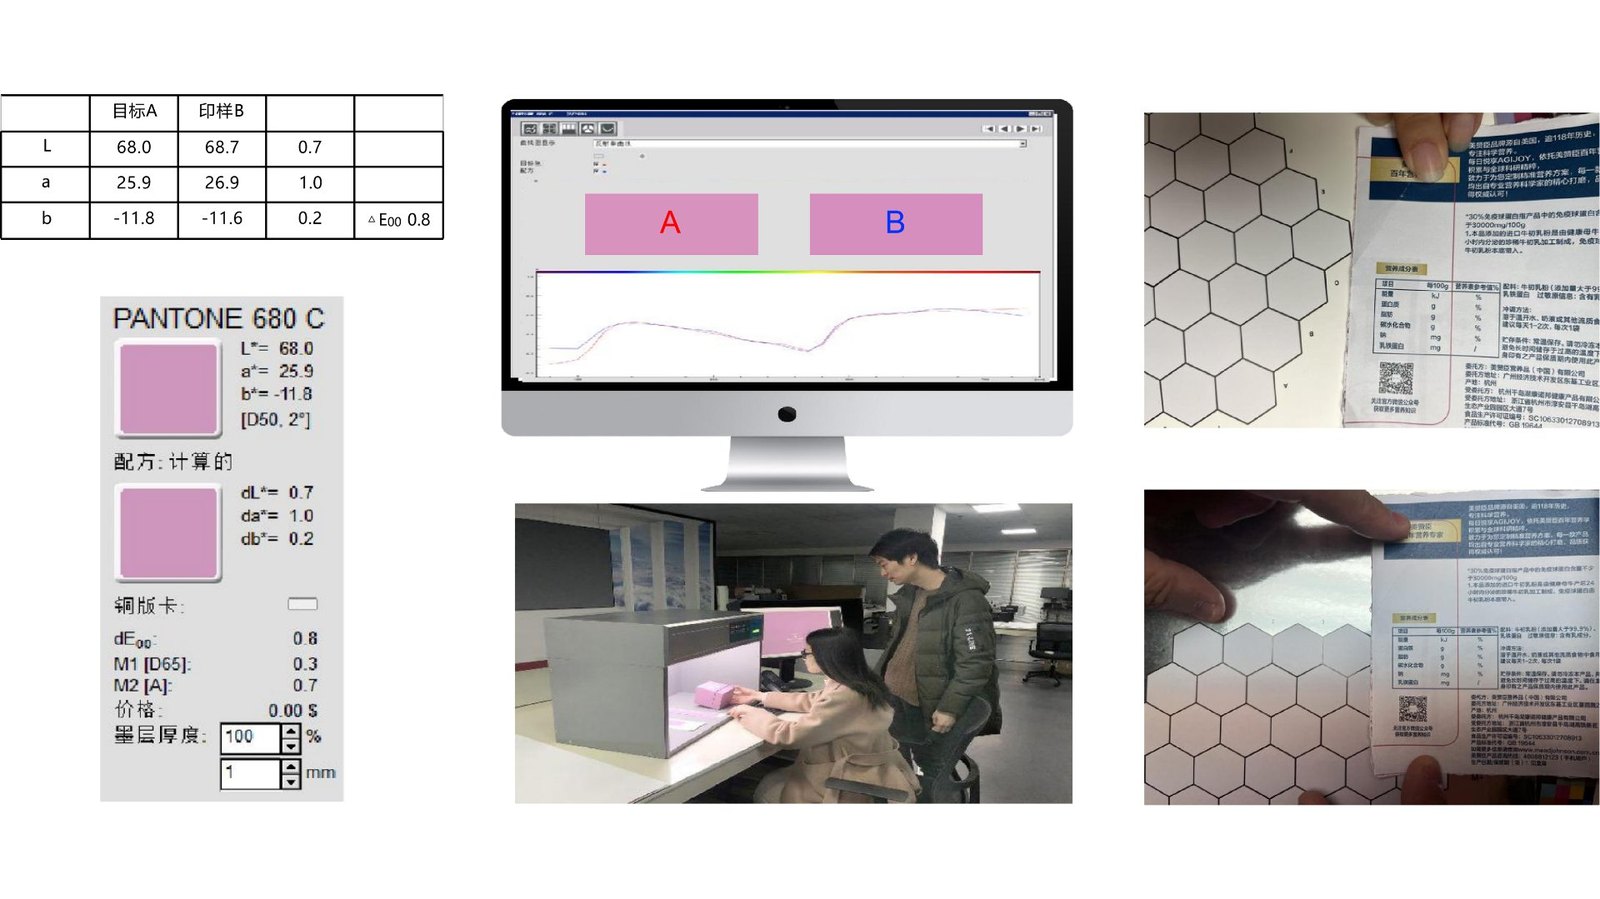
| project | objective A | Sample B | D-value |
|---|---|---|---|
| L | 68.0 | 68.7 | 0.7 |
| a | 25.9 | 26.9 | 1.0 |
| b | -11.8 | -11.6 | 0.2 |
Overall color difference: △E00 0.8. For the same spot color, precise color matching across different materials is achieved in accordance with customer requirements, ensuring consistent color rendering.
Mass Production Restorability · Brand Color Consistency Management
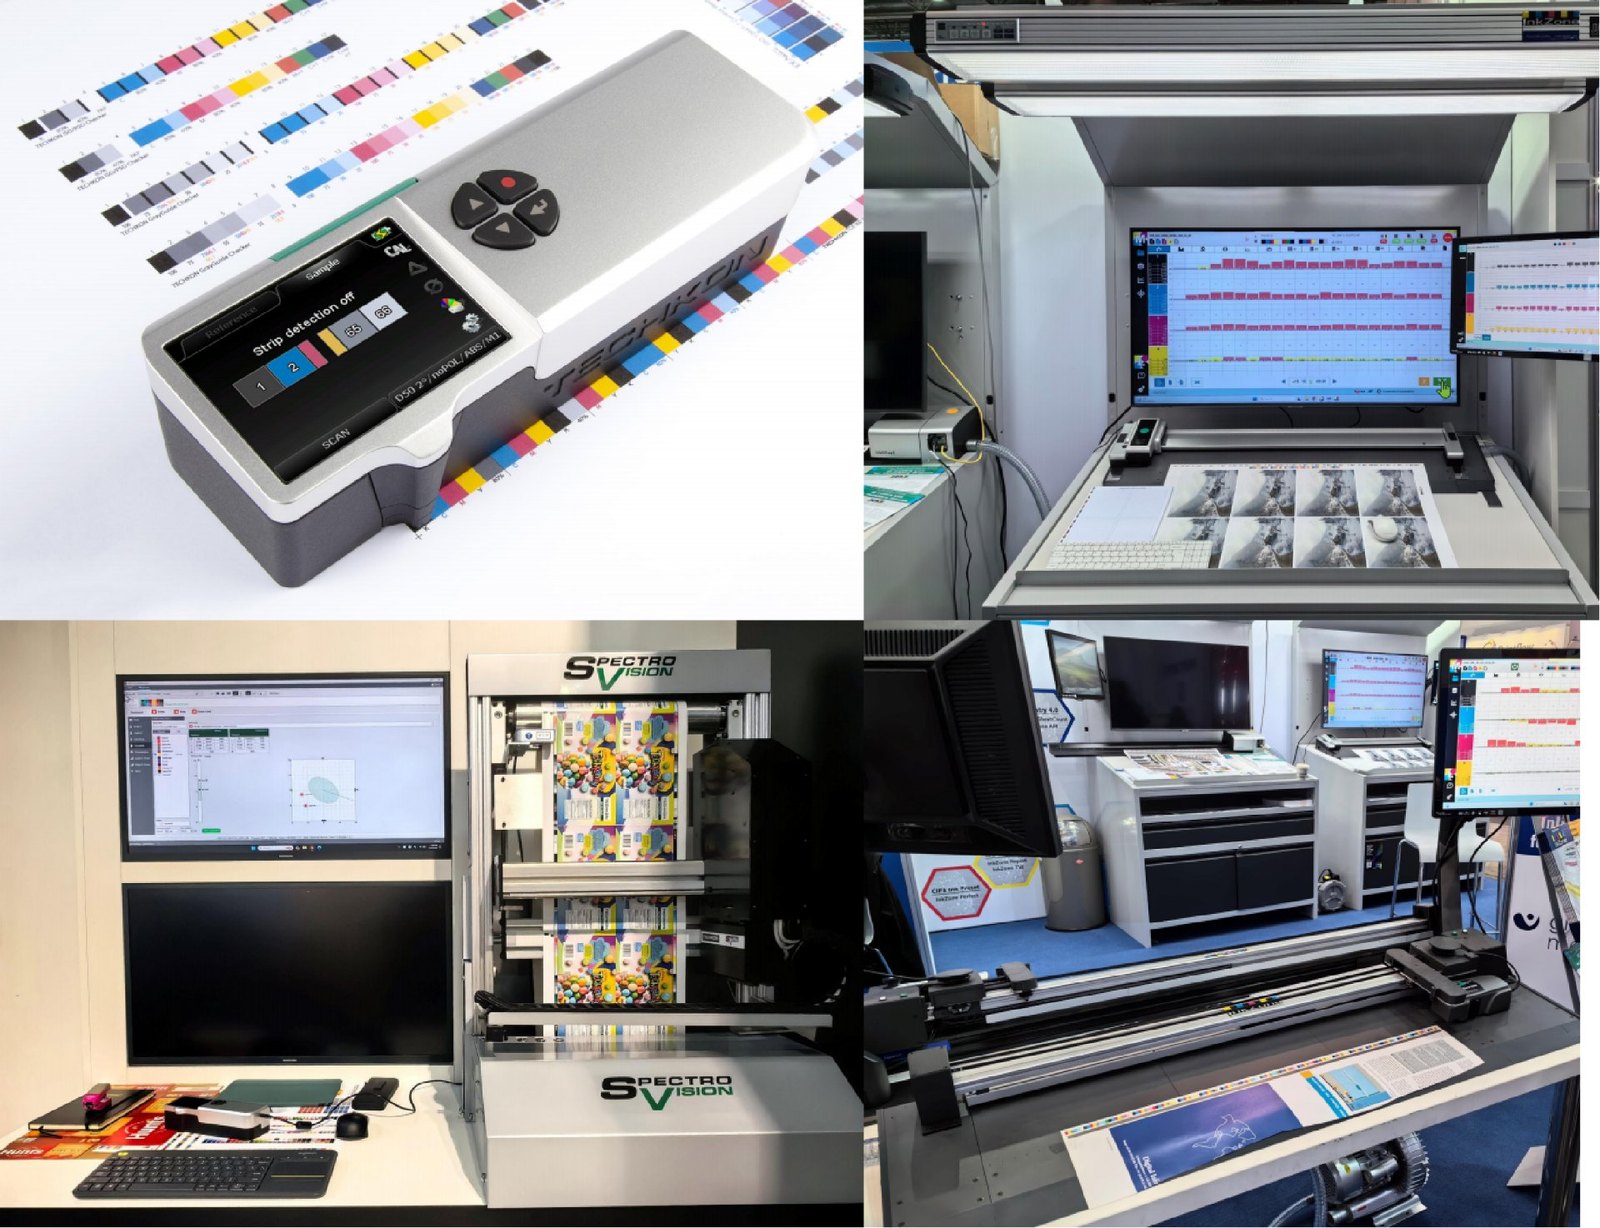
Professional color equipment digitizes, standardizes, and normalizes packaging color data, enabling brands to achieve consistency between digital packaging colors and the final production results in the factory.
Case Study—Dongpeng Buhui La Establishes Brand Color Standards
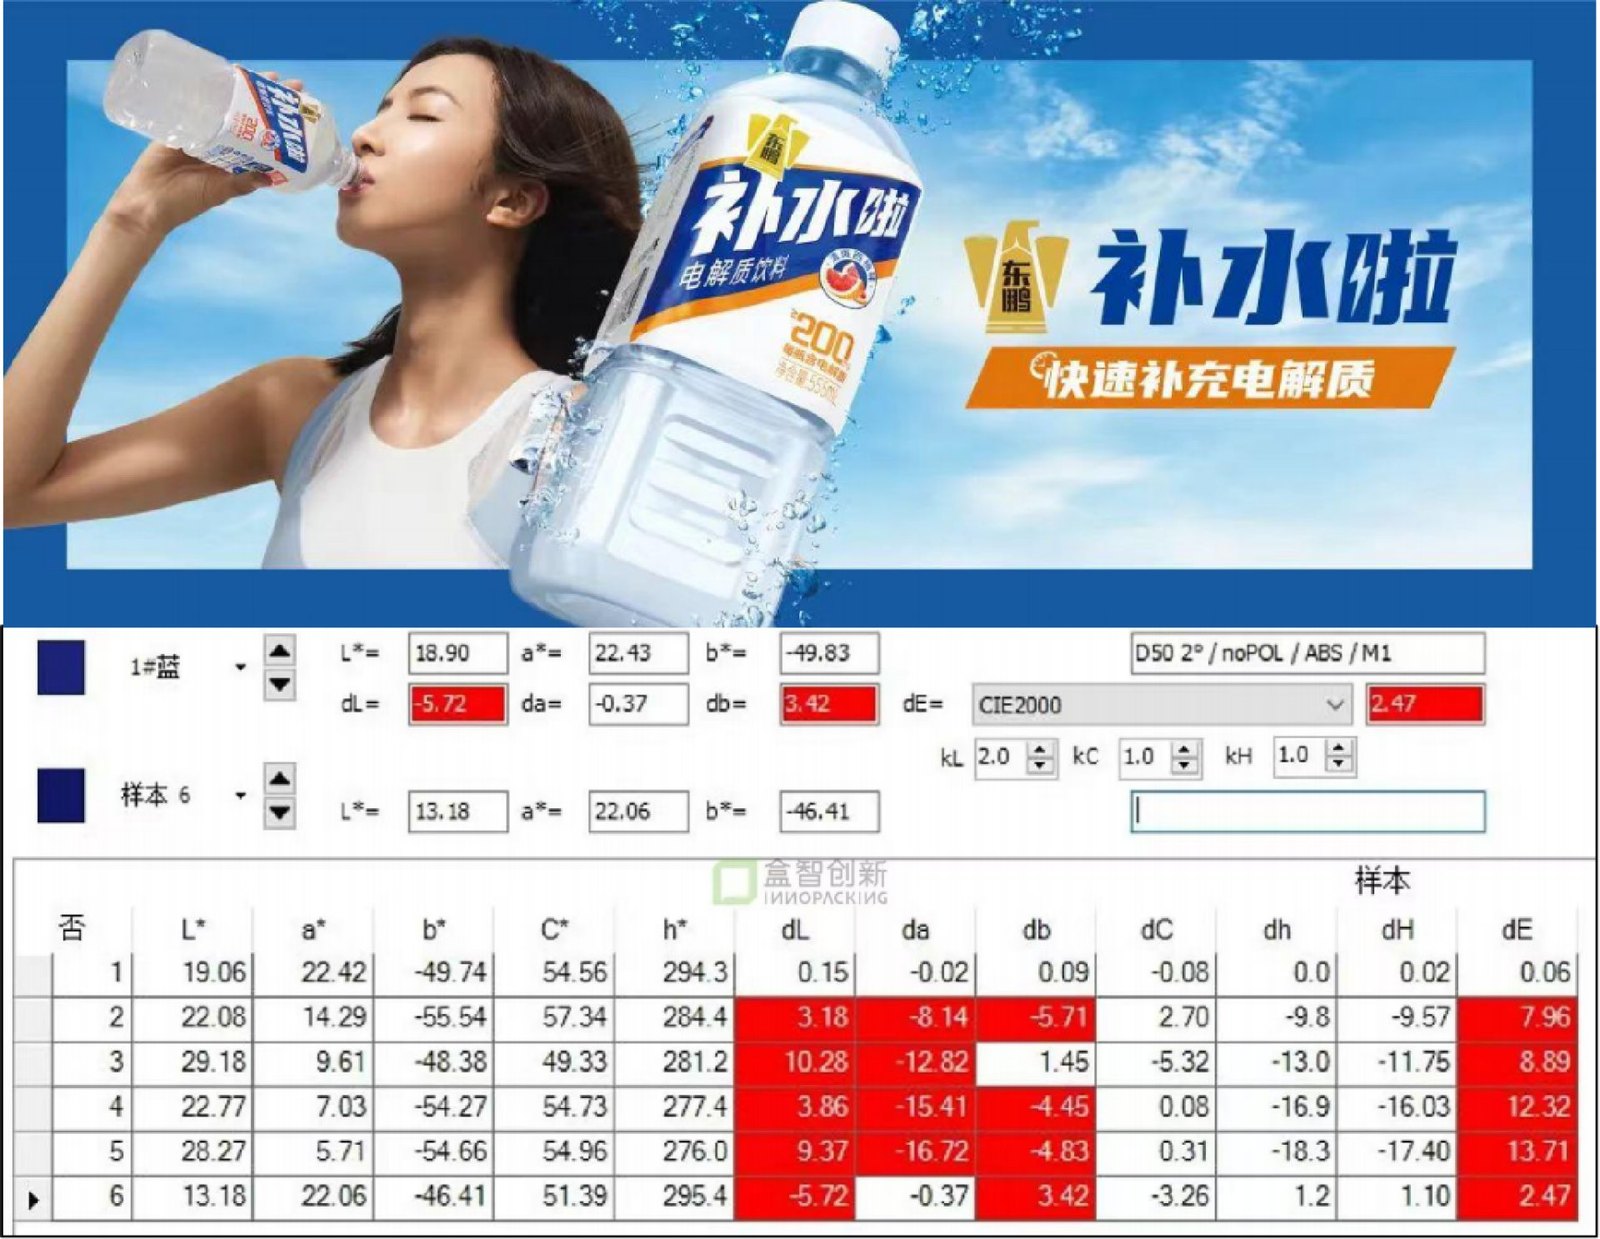
- The color samples provided by six different suppliers exhibit significant color variations.
- INNOPACKING has established a unified digital color standard and a sample catalog.
Digital samples and factory color matching
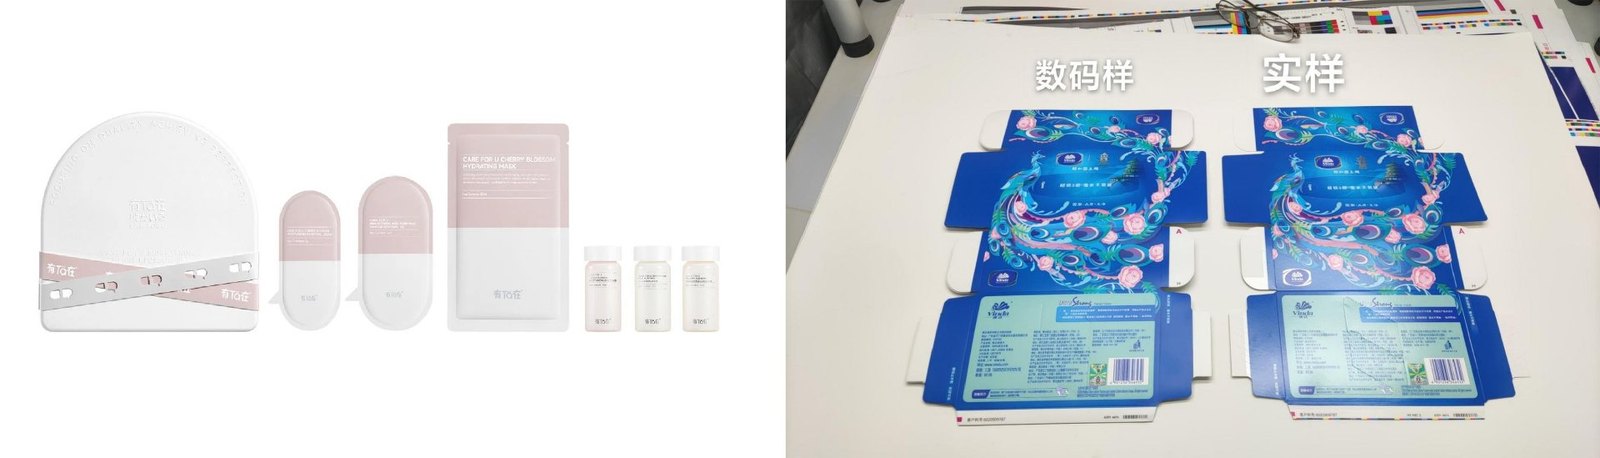
After INNOPACKING digital samples were matched with the factory's color palette, the proofing results were excellent and exhibited high color fidelity.
Would you like to learn how this capability can be implemented in your project?Start a Project ↗